

 English
 中文简体
 русский
 Español
 عربى
Modular Photovoltaic Cabin Manufacturer: The Power Station That Arrives Assembled
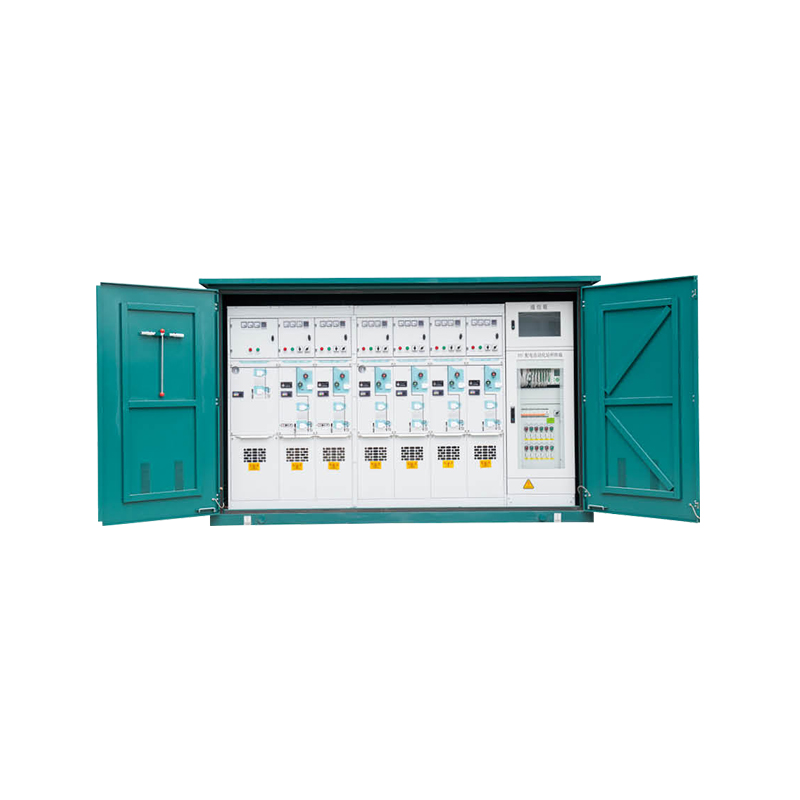
A solar farm needs inverters, transformers, switchgear, and a weatherproof place to put them. On-site construction takes months. A modular photovoltaic cabin manufacturer builds the enclosure in the factory, mounts the equipment inside, runs the wiring, and tests the system before the cabin ships. The cabin lands on a prepared pad, connects to the arrays and the grid, and powers up. The site work that used to take a construction crew weeks turns into a connection job measured in days.
Factory Wiring Beats Field Wiring
The cables inside the cabin are cut to length and terminated under controlled conditions. The protection relays are programmed and tested. The interconnections between the inverter, the transformer, and the switchgear are made on the factory floor, where the temperature is stable and the dust is controlled.
A modular photovoltaic cabin manufacturer that tests the full system before shipment catches the loose terminal and the mislabeled conductor before the cabin leaves. Field wiring errors are expensive because the crew is on site, the equipment is energized, and the schedule is already tight.
The Thermal Problem in a Steel Box
Inverters and transformers generate heat. A sealed steel enclosure in direct sun turns into an oven without a thermal design. The cabin needs ventilation, forced air, or air conditioning, depending on the internal heat load and the local climate.
A modular photovoltaic cabin manufacturer sizes the cooling for the heat rejection of the equipment plus the solar gain on the enclosure. Insulated sandwich panels form the walls and the roof, reducing the thermal load from the sun. The cabin that keeps the equipment within its rated temperature range avoids the derating and the shutdowns that cost production in the summer.
Modular Sections and Site Assembly
The cabin is built in sections that ship on standard trucks and bolt together on site without a heavy crane. A small rooftop system uses one section. A utility-scale farm uses multiple identical sections, so the site team repeats the same installation process at each pad.
Sealing and Cable Entry
The cabin has to keep the rain, the dust, and the insects out. The door gaskets, the panel joints, and the cable entry glands are all part of the seal. The cable entry goes through the bottom, with the weatherproof glands, so the water does not track along the cable into the enclosure.
A modular photovoltaic cabin manufacturer that tests the completed cabin for weather tightness, not just the individual panels, catches the leak at the joint before the cabin ships.
What the factory has to deliver:
- Factory-integrated inverter, transformer, and switchgear
- Protection settings programmed and tested before shipment
- Thermal management sized for the equipment and the climate
- Insulated sandwich panel construction
- Modular sections that ship and assemble without a crane
- Weather-tightness tested on the completed cabin
Where the Cabin Goes
The commercial rooftop uses the small cabin next to the building. The utility-scale farm uses the dozens of identical cabins across the site. The energy storage project uses the cabin with the battery racking and the fire suppression built in.
When the Cabin Fails
The cabin leaks at the door seal and the water reaches the switchgear. The cooling is undersized and the inverter derates at noon. The site wiring takes weeks because the factory wiring was incomplete. Each one is a decision made at the design and the factory stage, not on the site.
Next
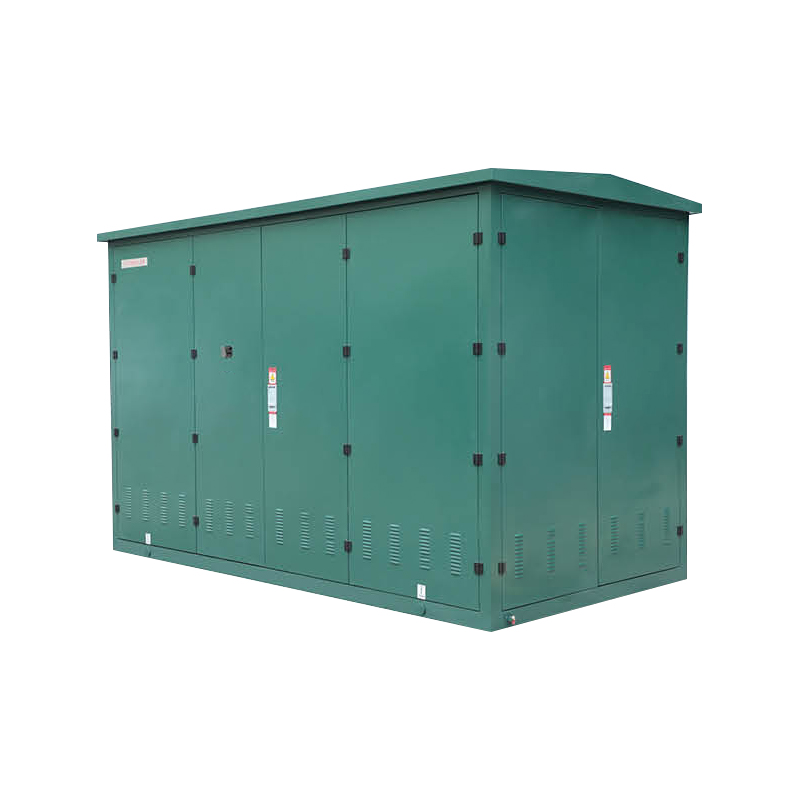
Outdoor Rust Proof 10kV Cable Branch Box Factory: The Enclosure That Keeps Medium Voltage Dry
<p>A 10kV cable branch box sits at the junction where one underground cable splits into severa...
View More
- PRODUCTS
- New Energy Power Distribution Equipment
- Box Type Substation
- Cable Branch Box/Switch Station
- High Voltage Switchgear
- Low Voltage Switchgear
- Engineering Vacuum Circuit Breaker
- New Energy Vehicle Floor Charging Pile
- Commercial Energy Storage
- Photovoltaic Complete Box
- High Voltage Arrester
- INFORMATION
-
-
Phone+86-13868788848
+86-13356188725 -
Tel+86-0577-88810567
-
E-mail
-
AddNo. 59, Youyi Road, Xinguang Industrial Zone, Liushi Town, Yueqing City, Zhejiang, China
-
- ENQUIRE WITH US
Photovoltaic Module Manufacturer

